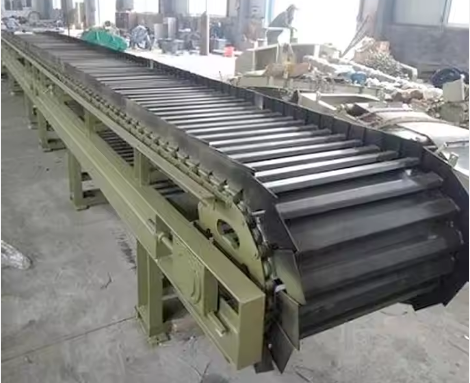
A bucket conveyor is a material-handling system designed to lift and transport bulk materials vertically or at steep inclines using a series of buckets attached to a belt or chain.
Key features
- Vertical/high-angle conveying: Efficiently moves materials between different elevations.
- Enclosed material flow: Reduces dust, spillage, and material loss.
- Continuous operation: Suitable for high-volume, continuous material handling.
- Flexible capacity: Available in different bucket sizes, speeds, and configurations.
Typical applications
Bucket conveyors are commonly used for:
- Grains, cereals, and seeds
- Cement, clinker, and minerals
- Fertilizers and chemicals
- Food and agricultural products
- Coal and other bulk solids
- Powders, pellets, and granules
Advantages
- Small floor-space requirement
- High vertical lifting capability
- Good throughput and energy efficiency
- Relatively enclosed and clean operation
- Suitable for long-term automated material handling