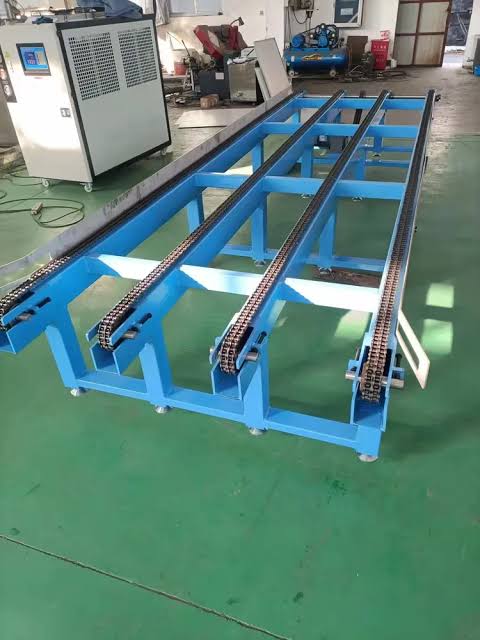
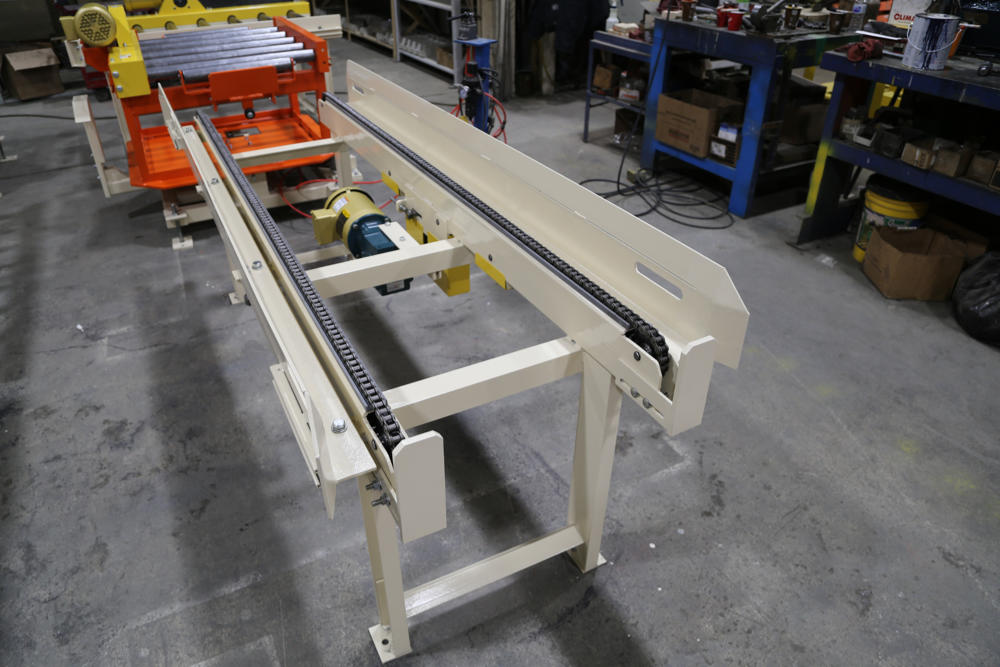
A chain conveyor is a material-handling system that uses one or more continuous chains to move materials from one location to another. It is particularly suitable for heavy, bulky, or palletized loads.
Key Features
- Handles heavy loads with high durability.
- Suitable for pallets, containers, boxes, and industrial components.
- Can operate in horizontal or inclined configurations.
- Provides controlled and reliable movement.
- Requires relatively low maintenance when properly lubricated.
Advantages
- High load-carrying capacity.
- Robust construction and long service life.
- Effective in harsh industrial environments.
- Can be integrated with automated production and storage systems.
- Allows accumulation and controlled transfer of materials.
Applications
Chain conveyors are widely used in manufacturing plants, warehouses, automotive industries, assembly lines, and distribution centers.